The Complete Guide to Metalworking Fluids: Cutting, Grinding, and Forming
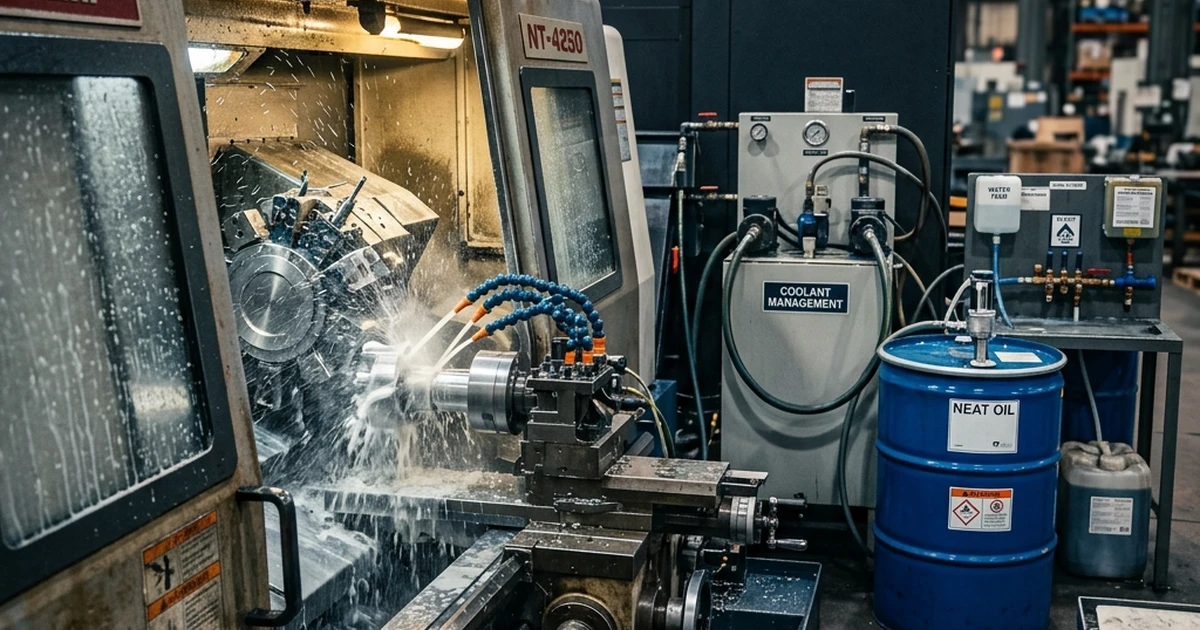
Metalworking fluids are one of the most operationally critical consumables in precision manufacturing, yet they are frequently underspecified and poorly maintained. The term encompasses a broad family of cutting fluids, grinding fluids, and forming lubricants — each engineered to reduce friction, dissipate heat, flush swarf, and protect metal surfaces during machining and shaping operations. Choosing the wrong fluid or neglecting sump maintenance can cost an operation far more in tool wear, scrap rates, and downtime than the fluid itself is worth. This comprehensive guide covers everything from the fundamental chemistry of metalworking fluid formulation through to type classification, selection logic, maintenance protocols, health and safety obligations, and industry trends — providing the definitive technical reference for engineers, production managers, and formulation specialists alike.
What Are Metalworking Fluids and Why They Matter in Industry
Metalworking fluids (MWFs) are liquid media applied at or near the tool-workpiece interface during metal cutting, grinding, honing, and forming operations. Their primary purpose is to manage the extreme thermal and tribological conditions that arise when metal is sheared, deformed, or abraded at high speed. Without effective fluid management, tool temperatures can exceed the thermal stability of cutting inserts, workpiece surfaces can sustain thermal damage that degrades dimensional tolerance, and swarf accumulation can cause re-cutting and surface finish deterioration.
The global metalworking fluid market exceeds several billion dollars annually, reflecting the scale of machining operations in automotive, aerospace, general engineering, and energy sectors. In a typical automotive engine machining line, MWF system costs — including fluid purchase, treatment, and disposal — represent a significant fraction of total component manufacturing cost. When a fluid is correctly selected and managed, it can extend cutting tool life by 50–200%, improve surface finish consistency, and protect machine tool slideways and spindles from corrosion between shifts.
Metalworking fluids also carry substantial health and environmental responsibilities. Workers exposed to mist or aerosol from MWF sumps face risks of dermatitis, respiratory sensitisation, and, in poorly managed systems, bacterial-associated lung disease. Regulatory frameworks in the EU, UK, and US impose strict exposure limits, monitoring requirements, and disposal obligations on MWF users. Understanding the full scope of metalworking fluid technology — from chemistry to compliance — is therefore essential for any manufacturing engineer or production facility manager.
The Science Behind Metalworking Fluids: Key Chemistry and Mechanisms
At the tool-workpiece interface, three distinct but interacting mechanisms must be managed simultaneously: heat generation from plastic deformation and friction, tribological contact between tool and workpiece under extreme pressure, and chip or swarf removal from the cutting zone. Metalworking fluid chemistry is engineered to address all three through a combination of base fluids, lubricity additives, extreme-pressure (EP) agents, corrosion inhibitors, biocides, emulsifiers, and foam-control agents.
In water-miscible systems, the thermal mass and high heat capacity of water gives these fluids a strong cooling advantage over straight oils. Emulsifiers — typically anionic or non-ionic surfactants — stabilise mineral or synthetic oil droplets in the water phase, creating the characteristic milky appearance of soluble oils. Semi-synthetic and synthetic fluids reduce or eliminate the mineral oil content, relying on synthetic lubricity agents such as fatty acid esters, polyalkylene glycols, or synthetic sulfonates to maintain tribological performance. EP additives, principally chlorinated paraffins, sulphurised fatty acids, and phosphorus compounds, react with the metal surface under high contact pressures to form sacrificial boundary films that prevent metal-to-metal welding and reduce tool wear.
In neat oils, the base fluid — typically a naphthenic or paraffinic mineral oil, or a synthetic ester — carries the additive package without dilution. The viscosity of the neat oil must be matched to the machining operation: low-viscosity oils for high-speed operations where cooling by splashing is important, higher-viscosity oils for slow, high-load threading and broaching where the lubricant film must persist under heavy contact. Corrosion inhibition is achieved through alkaline reserve (in water-miscible fluids, maintained via pH buffering with alkanolamines or borates) or through adsorption-type inhibitors in neat oils that form a protective film on freshly machined steel surfaces.
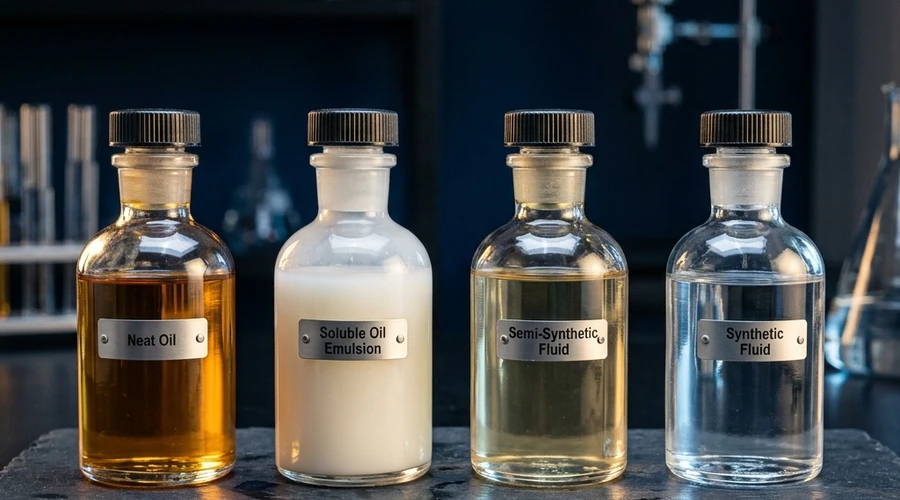
The four principal metalworking fluid types — from left: neat oil (amber, undiluted), soluble oil emulsion (milky white), semi-synthetic (translucent), and synthetic (water-clear) — each suited to distinct machining conditions and performance requirements.
Types and Classification: A Complete Overview of Metalworking Fluids
The most widely used classification system for metalworking fluids divides them into four principal categories based on their composition and the role of water in the system. ISO 6743-7 provides the internationally recognised classification framework used across manufacturing industries globally. Understanding these categories — and the performance trade-offs between them — is the starting point for any fluid selection decision.
| Type | ISO Class | Composition | Cooling Ability | Lubrication Ability | Typical Applications |
|---|---|---|---|---|---|
| Neat (Straight) Oil | MH / MHH | Mineral or synthetic oil + EP/lubricity additives, no water dilution | Low | Excellent | Gear hobbing, threading, broaching, deep-hole drilling, grinding sensitive alloys |
| Soluble Oil (Emulsifiable Oil) | MAE / MAEF | Mineral oil + emulsifiers, diluted in water (3–10% oil in use) | Good | Good | General turning, milling, drilling on ferrous metals; heavy-duty operations |
| Semi-Synthetic Fluid | MAC / MACF | Low mineral oil content + synthetic lubricity agents + emulsifiers, water-diluted | Very Good | Good | High-speed CNC machining, grinding, multi-metal operations, aluminium |
| Synthetic Fluid | MB / MBF | No mineral oil; synthetic lubricity agents (PAG, esters), water-diluted | Excellent | Moderate–Good | Precision grinding, high-speed machining, hard alloys, clean-room environments |
| Forming / Drawing Fluid | MG / MGH | Neat or emulsifiable; heavy EP additive package, high viscosity index | Low–Moderate | Excellent | Deep drawing, stamping, wire drawing, roll forming, extrusion |
Key Performance Properties and Specifications
Selecting and managing a metalworking fluid requires monitoring a set of performance parameters that indicate both process effectiveness and fluid health. These properties must be evaluated at commissioning, during routine sump management, and when problems arise. They are also the basis for supplier product testing and approval, and for meeting the requirements of customer quality management systems in aerospace and automotive supply chains.
| Property | Test Method | Significance for MWF Performance |
|---|---|---|
| Kinematic Viscosity | ISO 3104 / ASTM D445 | Controls film thickness and flow at the cutting zone; too high impairs chip flushing, too low reduces lubricant film under load |
| pH (in-use emulsion) | ISO 4316 / ASTM E70 | Indicator of alkaline reserve; most water-miscible MWFs require pH 8.5–9.5 to inhibit microbial growth and prevent corrosion |
| Concentration (Brix) | Refractometer / ISO 6743-7 | Ensures correct dilution; under-concentration causes corrosion and tool wear; over-concentration causes foam, skin irritation, and waste |
| Emulsion Stability | ASTM D1401 / CEC L-40 | Confirms emulsifier package maintains stable oil-in-water dispersion across water hardness and temperature ranges encountered in use |
| Extreme Pressure Performance | IP 239 / ASTM D2783 (4-ball EP) | Measures load-carrying capacity of EP additives; critical for heavy-duty turning, gear grinding, and forming applications |
| Corrosion Inhibition (Cast Iron) | ASTM D4627 / Herbert Corrosion | Verifies protection of ferrous workpieces and machine components in contact with aqueous fluid during and between shifts |
| Microbial Count (TVC) | ASTM E2694 / IP 385 | Total viable count; action levels typically <10³ CFU/mL; counts >10⁶ CFU/mL indicate sump failure requiring treatment or disposal |
| Foaming Tendency | ASTM D892 / DIN 51566 | Excessive foam in high-speed operations impairs cooling, causes overflow, and indicates surfactant imbalance or tramp oil contamination |
Selection Guide: Matching Metalworking Fluid to Operation and Material
No single fluid type suits all machining operations or all workpiece materials. The selection decision depends on a matrix of factors: the severity and nature of the machining operation (cutting speed, feed rate, depth of cut), the workpiece material, the machine tool type and configuration, the metals in contact with the fluid (including fixtures and machine components), regulatory constraints on fluid chemistry, and the cost of sump management for the chosen fluid type. The following framework guides the key decisions.
Operation severity is the first filter. Grinding operations generate more heat per unit of metal removed than turning or milling, making cooling the dominant requirement — which favours synthetic or semi-synthetic fluids with high water content. In contrast, gear hobbing or thread whirling at low speeds under high contact pressure demands maximum lubrication, pointing to neat oil with a heavy EP additive package. Multi-operation machining centres that perform turning, drilling, and tapping in a single setup benefit from balanced semi-synthetic fluids that provide acceptable lubrication across all operations without requiring tool-specific fluid changes.
Material compatibility is critical. Aluminium and its alloys are sensitive to staining and chemical attack from high-pH amine-based fluids; dedicated aluminium-compatible semi-synthetics with controlled pH and without strongly alkaline components are required. Copper and copper alloys are attacked by sulphurised EP additives — specifying EP-free or copper-compatible fluid is non-negotiable. Titanium and nickel superalloys require high-pressure, high-volume coolant delivery to manage the extreme temperatures generated by their low thermal conductivity. Cast iron, which produces fine graphite-contaminated fines, demands fluids with robust filtration tolerance and strong corrosion inhibition.
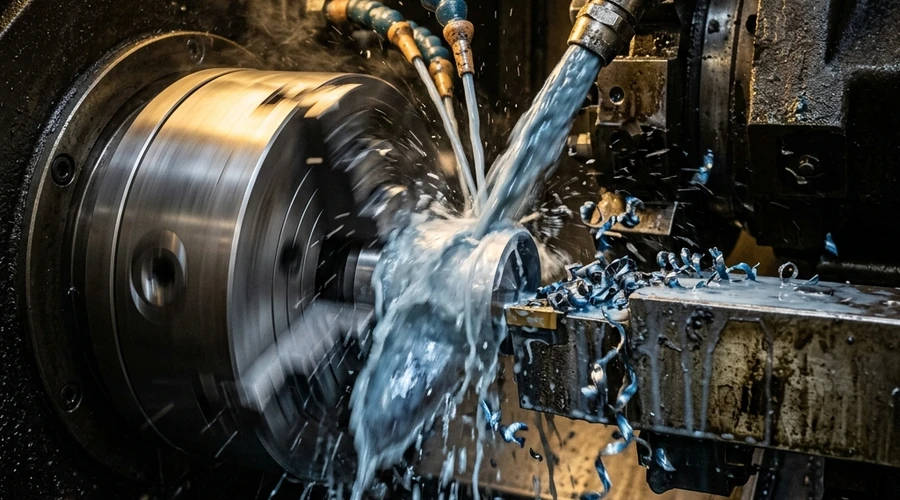
High-pressure flood cooling at the cutting insert-workpiece interface — the cornerstone of effective metalworking fluid delivery in modern CNC turning operations, removing heat and evacuating chips simultaneously.
Sump Management and Fluid Maintenance
The performance and longevity of a water-miscible metalworking fluid is determined not just by its formulation at the point of purchase, but by how well it is managed throughout its service life. Sump management — the ongoing monitoring and maintenance of the fluid system — is where the majority of metalworking fluid problems originate. A correctly formulated but poorly maintained fluid will fail faster and cause more production problems than a modest fluid that is conscientiously managed.
The key maintenance tasks are: daily concentration checks using a calibrated refractometer; daily or shift pH measurement; tramp oil removal using skimmers or coalescers (tramp oil from machine slideways and hydraulic leaks is the primary vector for microbial contamination by providing anaerobic micro-environments); periodic biocide treatment at intervals specified by the fluid supplier and in the site COSHH assessment; and complete sump clean-out and recharge at intervals determined by fluid life and microbial monitoring data. Machine tool filters, chip conveyors, and coolant return lines must be kept clear to prevent stagnation zones. Water quality used for dilution is also critical — water that is too hard causes emulsion instability and calcium soap deposits; excessively soft water can cause foaming and pH instability.
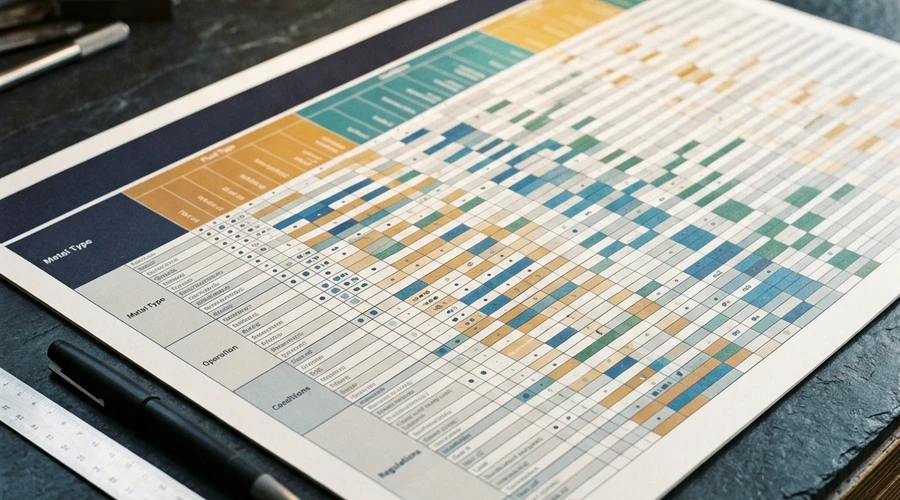
A metalworking fluid selection matrix maps metal type, machining operation, speed-load regime, and regulatory environment to the appropriate fluid category — from neat oil for maximum EP performance to synthetic for maximum cooling in precision grinding.
Testing Methods and Industry Standards for Metalworking Fluids
Metalworking fluids are subject to a comprehensive framework of international and national standards that govern product testing, classification, workplace exposure, and disposal. The ISO 6743-7 standard provides the primary product classification system, defining fluid types and their minimum performance requirements. The ISO 15488 standard addresses safety requirements for metalworking fluids, while national regulations — HSE EH40 in the UK, OSHA PELs in the US, and TRGS 611 in Germany — specify occupational exposure limits for mist and aerosol. Quality-critical sectors such as aerospace (Nadcap accreditation) and automotive (IATF 16949) impose additional fluid qualification requirements through customer-specific specifications.
| Standard / Method | Scope | What It Measures |
|---|---|---|
| ISO 6743-7 | Product classification | Defines MWF types (MH, MAE, MAC, MB, MG) and performance requirements by category |
| ASTM D2783 / IP 239 | EP performance | Four-ball EP weld load and wear scar measurement under increasing contact load |
| ASTM D1401 | Emulsion stability | Demulsibility — how quickly a water-miscible fluid separates from mineral oil contamination |
| ASTM D4627 | Corrosion protection | Cast iron chip corrosion test — evaluates corrosion inhibitor protection of ferrous metal swarf and components |
| ASTM E2694 / IP 385 | Microbial control | Total viable count of bacteria; used in sump monitoring programmes with action levels defined in COSHH assessments |
| HSE EH40 / OSHA 1910.1000 | Occupational exposure | Workplace exposure limits for mineral oil mist (WEL: 1 mg/m³ 8hr TWA in UK); requires air monitoring in machining areas |
| TRGS 611 (Germany) | Biocide management | Regulates permissible biocide actives in water-miscible MWFs; excludes formaldehyde-releasing preservatives |
Health, Safety, and Regulatory Considerations
Metalworking fluids present a multi-pathway health risk that must be managed through a structured COSHH (Control of Substances Hazardous to Health) or equivalent risk assessment framework. The primary exposure routes are skin contact — leading to irritant or allergic contact dermatitis from surfactants, biocides, and amine-based corrosion inhibitors — and inhalation of aerosol mist generated by high-speed rotating components and high-pressure coolant delivery systems. A third route, ingestion via contaminated hands, is addressed through workplace hygiene protocols rather than fluid reformulation.
Biocide selection for water-miscible fluids is heavily regulated. In the EU, the Biocidal Products Regulation (BPR, Regulation 528/2012) requires that all biocide actives used in MWFs be authorised under Product Type 13. Formaldehyde-releasing preservatives such as hexahydrotriazines and benzimidazole-based actives are subject to increasing restriction and in some markets are banned outright. The preferred alternatives include isothiazolinone-based biocides, phenoxyethanol, and pyrithione salts — each with their own stability, spectrum, and regulatory profile that must be matched to the fluid type and sump conditions. In Germany, TRGS 611 provides a specific approved list of biocides for MWFs with concentration limits and exposure controls.
Mist enclosures, local exhaust ventilation (LEV), and biological health surveillance (spirometry for respiratory health, skin assessment for dermatitis) are mandatory controls in regulated environments handling large volumes of water-miscible MWFs. Coolant delivery system design — minimising splash zones and enclosing the cutting zone — is increasingly specified in new CNC machine tool procurement as a primary engineering control. Fluid disposal must comply with national effluent discharge consents; most water-miscible fluids require chemical or physical treatment (emulsion splitting, ultrafiltration) before discharge or must be collected by a licensed waste contractor for off-site treatment.
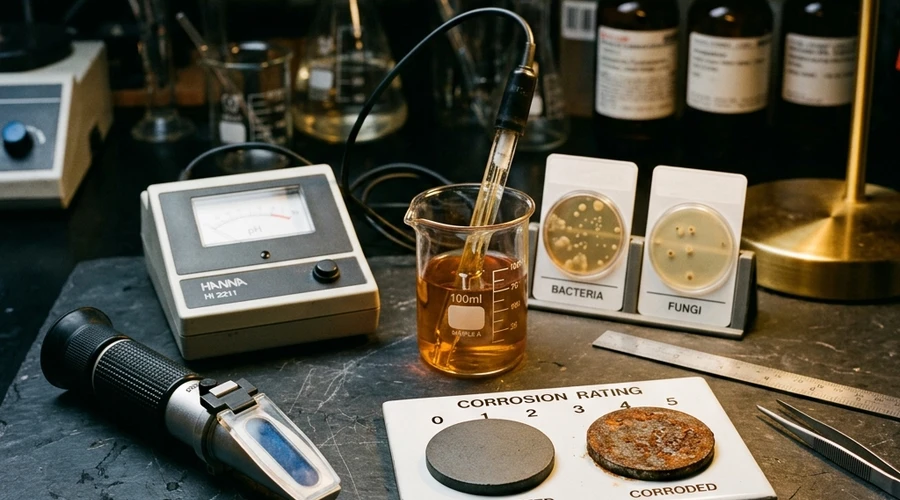
Routine sump monitoring combines refractometer concentration measurement, pH tracking, dip-slide microbial counting, and corrosion test panel assessment — the four pillars of a proactive MWF health management programme.
Common Metalworking Fluid Problems and How to Address Them
Despite advances in MWF formulation, a predictable set of failure modes recurs across manufacturing operations. Most arise from the interaction of the fluid with the machining environment — tramp oil ingress, water quality variation, temperature changes, and accumulated swarf — rather than from inherent formulation deficiencies. Understanding the root cause mechanism for each failure mode directs the appropriate corrective action. Detailed diagnosis of specific MWF problems and their formulation-level root causes is covered in the lubricants technical library and the broader cutting fluids guide.
Corrosion on workpieces or machine surfaces typically indicates pH drift below the effective range of the corrosion inhibitor package — most commonly caused by dilution of the concentrate by excessive water top-up without corresponding concentrate addition, or by bacterial acid production in a microbiologically compromised sump. Foaming is usually triggered by tramp oil contamination, excessively soft or hot water, or surfactant-laden coolant return lines that create turbulence. Emulsion instability and separation can be caused by high-hardness water forming calcium soaps that destabilise the emulsifier system, or by contamination with incompatible hydraulic fluids that displace the emulsifier from the oil-water interface.
Tool wear that deteriorates suddenly despite correct fluid delivery often points to EP additive depletion — the result of excessive dilution, high operating temperatures that degrade sulphur-phosphorus additives, or pH-driven hydrolysis of ester-based lubricity agents. Skin complaints among machine operators are the signal for an immediate review of biocide type and concentration (formaldehyde releasers are a common sensitiser), amine content (MEA and TEA can cause sensitisation), and the concentration of the in-use fluid — both under and over-concentration relative to the specification can trigger dermatitis. References to relevant regulatory guidance should be made through the NIOSH metalworking fluids resource page.
Industry Trends and Future Outlook for Metalworking Fluids
The metalworking fluid industry is undergoing structural change driven by three converging forces: tightening regulation of biocides and hazardous chemistry, the rapid adoption of minimum quantity lubrication (MQL) and near-dry machining in high-volume manufacturing, and the demand for fluids compatible with the advanced materials — titanium alloys, CFRP composites, metal matrix composites, and additively manufactured parts — that are increasingly central to aerospace and medical device supply chains.
Biocide-free or biocide-reduced water-miscible formulations are gaining traction, using a combination of hurdle technology — controlled pH, low available water activity, and non-biocidal antimicrobial components — to resist microbial contamination without relying on regulated preservatives. These systems are particularly attractive for automotive Tier 1 suppliers seeking to simplify REACH and BPR compliance. Simultaneously, MQL technology — delivering micro-droplets of neat lubricant in a compressed air stream directly to the cutting zone rather than flooding the machining area — is being adopted for high-volume aluminium and cast iron machining, dramatically reducing fluid consumption, mist generation, and sump management cost.
Sustainability requirements are also reshaping base fluid selection. Ester-based synthetics derived from renewable feedstocks — vegetable oil esters, biosynthetic esters — are entering commercial MWF formulations as alternatives to mineral oil components, supported by the broader industrial sustainability agenda and the growing availability of bio-based oleochemical feedstocks at competitive cost. In parallel, closed-loop fluid management systems that recycle, filter, and recondition spent fluid rather than disposing of it are becoming best practice in lean manufacturing environments, reducing both disposal costs and environmental impact. Engagement with both industry resources and our rust preventive oils guide provides further context on lubrication sustainability trends.
Frequently Asked Questions About Metalworking Fluids
What are metalworking fluids and why are they used?
What is the difference between neat cutting oil and water-miscible metalworking fluid?
What are the main types of metalworking fluids?
How often should metalworking fluid concentration be checked?
What causes metalworking fluid to go rancid and how is it prevented?
What health risks are associated with metalworking fluids?
How are metalworking fluids disposed of?
Need Expert Guidance on Metalworking Fluid Selection?
Our team provides end-to-end technical consultancy — from metalworking fluid specification and sump management protocol development through to COSHH compliance, health surveillance programme design, and fluid disposal strategy. For the commercial planning side, the Metalworking / Cutting Fluid Standard Project Report is a costed India-basis feasibility study — soluble, semi-synthetic and synthetic coolants, three investment configurations and a five-year financial model.
Get a Free Consultation