Tablet Defects: Capping, Lamination, Sticking, Picking
A tablet batch can leave the press looking sound and then split in the coating pan, on the packing line or in a patient's hand. The worst compression problems are hidden, because a tablet can carry an internal crack and still pass visual inspection. Tablet defects such as capping, lamination, sticking and picking have different mechanisms, so one fix can cure a defect and aggravate its neighbour. This guide explains each mechanism, the powder and press variables behind it, the tests that expose it and a troubleshooting sequence. It draws on open-access compaction research, pharmacopoeial chapters and ICH Q8(R2), with formulation support from Global Formulation.
Tablet Defects: Four Failure Modes, Two Families
Tablet defects fall into two families that need different fixes. Capping and lamination are failures of the compact itself, where stored elastic energy overcomes the bonds between particles. Sticking and picking are failures of adhesion, where powder prefers the punch to its neighbours. Treating them as one problem sends a team to the wrong lever, since a change that helps one family, such as more lubricant, can aggravate the other.
| Defect | What You See | Mechanism in the Sources |
|---|---|---|
| Capping | The top or bottom crown separates, during decompression or ejection | Elastic recovery builds tensile stress that exceeds the cohesive strength of the compact, as a press maker's technical article describes |
| Lamination | The tablet splits into layers along the band | Air entrapment, shear stress during unloading, or tensile stress at the centre of a biconvex tablet |
| Sticking | Powder adheres to the punch face | Bonding between API and punch is stronger than bonding between that API and its neighbours in the tablet |
| Picking | Powder is pulled out near debossed features | A specialised case of sticking |
The definition of lamination as a split along the band comes from Vreeman and Sun, who also distinguish it from capping. The picking definition comes from a Purdue dissertation on modelling picking. Capping and lamination come first, because the stress cycle behind them explains most of what follows.
The Compression Cycle: Where Elastic Stress Is Stored
A tablet is not finished when the pressure peaks. During unloading, the elastic strain stored in the compact is relieved axially as the punch is withdrawn and radially as the tablet leaves the die. That elastic recovery can create defects at ejection, or later during testing, packaging and shipping, as Vreeman and Sun note in their air-entrapment study. The compression cycle is therefore a stress budget, and every variable either adds to the budget or adds bonding to pay it.
The two Sun-lab papers cited here link capping and lamination to a long list of variables, which fall into five groups.
- Tooling — tooling design, the tolerance between punch and die, and punch cup volume.
- Press settings — tableting speed and the position of compression within the die.
- Powder behaviour — deformation characteristics, bulk density and plasticity.
- Stored stress — in-die elastic recovery, residual die wall pressure and Poisson's ratio.
- The compact — tablet thickness and tablet tensile strength.
Lamination or capping is also a common symptom of overcompression, although not always an observed one. Pressing harder is therefore a poor default response to a weak tablet. Among the variables above, air entrapment was long questioned and has since been demonstrated directly, so the next section sorts the mechanisms.
Capping and Lamination: Three Mechanisms and Their Fixes
Capping and lamination are often treated together, yet they are different failure patterns with different mechanisms. Researchers describe at least three lamination types: air entrapment (Type 1), shear stress during ejection (Type 2) and tensile stress at the centre of biconvex tablets (Type 3). The effectiveness of a fix depends on which type is present. A team that applies the wrong fix loses time and, with some fixes, throughput.
| Type | Mechanism | What the Studies Found | Lever Implied |
|---|---|---|---|
| Type 1: air entrapment | Air sealed in the compact expands on unloading | In a 2015 direct-visualisation study, spherical defects tied to air bubbles appeared just below the lamination pressure, and lamination pressure fell as compact thickness rose | Deaerate the powder bed, slow the press, or change the formulation or granulation |
| Type 2: shear on unloading | Shear stress develops during decompression and ejection | On a compaction simulator, symmetrical decompression gave capping on both faces and lamination, while fixing the lower punch suppressed lamination and loaded ejection eliminated both | Change the unloading conditions |
| Type 3: biconvex centre | Tensile stress at the centre of the band from residual die wall pressure and tablet shape | A numerical and experimental study found it favoured by a small band thickness and a high compaction pressure | Lower the compaction pressure and increase the band thickness |
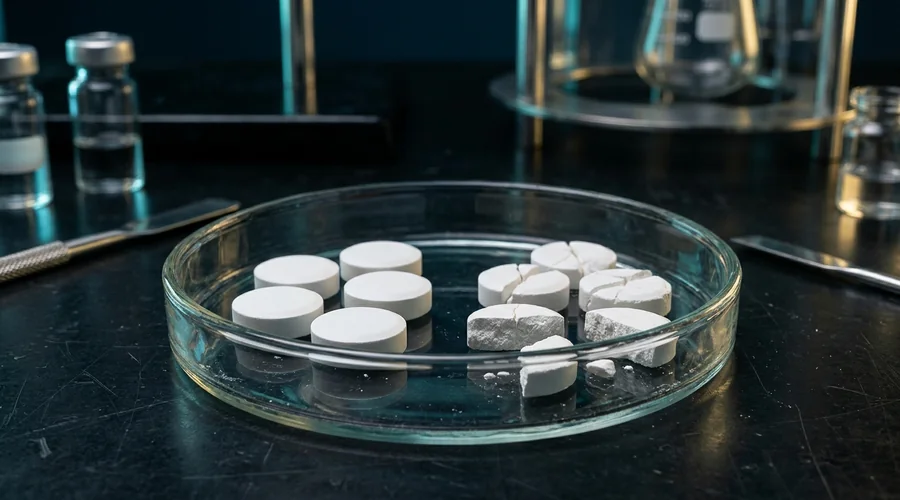
The Type 2 results come from model formulations on a simulator, so they show what unloading does, not that every rotary press behaves the same way. Their authors add that developing on eccentric presses can make defects hard to anticipate, especially lamination. The Type 3 crack forms at the centre and need not reach the surface, so it is easy to miss. Type 1 has the cleanest diagnosis, and the next section examines it.
Air Entrapment, Precompression and Hidden Cracks
Air entrapment is the mechanism you can measure before the tablet fails. When extensive plastic deformation seals the surface of the compact, air cannot escape, and it expands when pressure is released. Vreeman and Sun demonstrated this for celecoxib by comparing in-die elastic recovery with and without precompression. The method matters because the defects it exposes can sit inside tablets that look sound.
- Without precompression — elastic recovery fell from 4.5 to 2.1 percent between 20 and 100 MPa. It then rose to 13.5 percent at 200 MPa and peaked at 15.6 percent at 250 MPa.
- With precompression — a precompression pressure of 10 percent of the maximum removed the large increase, which points to air as the cause.
- Low pressure is enough — at a main pressure of 350 MPa, 5 MPa of precompression cut elastic recovery from about 14 to about 4 percent. Higher precompression lowered it only slightly.
- Strength — tablets were stronger at every pressure with precompression, and without it the breaking force dropped at 350 MPa.
In a follow-up study, the same group built a strategy that exaggerates air entrapment with high speed and high main pressure. It then records in-die elastic recovery against precompression pressure, and the pressure with the lowest recovery removes air best. A blend that laminated straight after ejection without precompression gave intact tablets across a wide range of high main pressures with it. Intact tablets are not needed to find the optimum, because the measurement happens inside the die.
The follow-up study lists what makes Type 1 lamination worse and what the options cost.
- Low bulk density — a high initial air content gives more air to trap.
- High plasticity — plastic powders seal their pores more readily.
- Low clearance — a tight fit between punch and die makes it harder for air to escape.
- Deep cups — punches with a large cup volume can force air into the compact.
- Slower speed or longer dwell — more time for air to escape, at the cost of throughput.
- Reformulation or better granulation — effective, but impractical late in development when the composition is locked.
- Precompression — convenient, keeps throughput and is available on most rotary presses.
Granule structure and excipient choice change how much air a powder holds, so our posts on pharmaceutical granulation technology and excipient selection for oral solid dosage forms cover those levers. Air is one stress source. Adhesion defects start from a different place, the tooling surface.
Tablet Sticking: Why Powder Prefers the Punch
Punch sticking is the adherence of powder to the tooling surface during compaction, and it leads to tablet defects, low efficiency and, in the worst cases, loss of batches. Xiang and Sun describe it as a contest of forces: sticking occurs when an API particle bonds more strongly to the punch than to its neighbours in the tablet. With repeated compression, the build-up is a monolayer when the force between adhered and fresh API particles is below that to neighbouring excipient particles. It is a multilayer when the force is above it.
- Surface area and tensile strength — in a statistical analysis of 24 compounds, particle surface area and tablet tensile strength were the most significant factors. Die-wall pressure, ejection force and take-off force correlated less.
- Thermal softening — a 2026 review of punch sticking notes that low-melting compounds soften under frictional heat.
- Hygroscopicity — the same review links it to adhesive capillary bridges.
- Ductility — high ductility increases the effective contact area, according to that review.
- Punch surface — in a study of five punch surfaces, microcrystalline cellulose adhered to titanium-nitride and uncoated steel punches after five hours although roughness was similar.
The punch-surface study explains the result through surface chemistry. Surfaces that stuck had a higher Lewis base surface-energy component and more polar functional groups and oxides. Its authors attribute sticking to capillary adhesion by water that evaporates from the powder bed during compression.
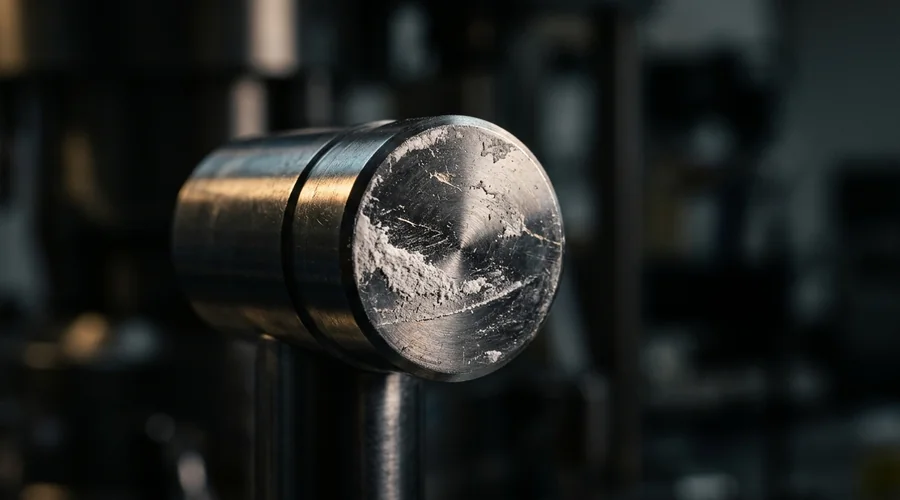
Xiang and Sun group the countermeasures into three categories, and the grouping works as a checklist.
- API engineering — salts and cocrystals, particle size and morphology, and holding the API in a porous carrier.
- Process parameters — compaction pressure and tooling design.
- Formulation design — different excipients, lower API loading and a changed lubricant level.
Lubricant level sits in the third category, but lubrication is the most double-edged lever in tableting, as the next section shows.
Lubricants: The Magnesium Stearate Trade-Off
Lubricants preserve tooling by reducing die-wall friction, which lowers ejection force and helps against sticking. They also cost something. Paul and Sun compared magnesium stearate, sodium stearyl fumarate and stearic acid in plastic and brittle matrices, and note that lubrication often prolongs disintegration, slows dissolution and reduces mechanical strength. The choice and level of lubricant is therefore a balance, not a default.
| Route | Benefit | Cost or Risk |
|---|---|---|
| Internal blend of magnesium stearate | Lower die-wall friction and ejection force | Lower tensile strength, and longer disintegration and dissolution in many formulations |
| External lubrication of the tooling | In a simulator study, equal or lower ejection force with less lubricant, and no loss of tensile strength or disintegration time | Can worsen sticking for some powders at low compaction pressure |
| Feed frame shear | None intended | Acts as extra internal lubrication and can cost tensile strength on scale-up |
The external-lubrication finding came from the Xiang and Sun study, which proposes a new force model for lubricated punches. A 2026 compaction-simulator study found that feed frame shear acting as extra lubrication played a major role in the tensile strength lost during scale-up. Shorter dwell time mattered little, with lubricated starch the exception. The authors suggest feed-frame-focused strategies to hold strength, and our post on dissolution method development covers how lubrication shows up in release. Lubricants act on the band and the punch face together, and the next defect is decided at the punch face.
Picking, Tooling Surfaces and Punch Design
Picking is a more specialised case of sticking, where powder is pulled away from the compact near debossed features. The Purdue dissertation describes the industry solution as trial and error, which it calls expensive, labour intensive and time consuming. Its finite-element model in Abaqus predicts picking and was used to study the stroke angle and degree of pre-pick of debossed features, and the influence of lubricant. The practical message is that engraving geometry and lubrication both enter the picking problem.
The sources name several tooling levers, and they cut across both defect families.
- Punch surface — coating choice changed sticking in the cellulose study above.
- Debossing geometry — stroke angle and pre-pick are inputs to the picking model.
- Cup volume — deep cups can push air into the compact and promote Type 1 lamination.
- Punch-die clearance — low clearance makes it harder for air to escape.
Coated tablets have their own sticking and picking in the pan, which our post on tablet coating technology covers. Tooling and press settings behave differently at scale, which is where many of these defects first appear.
Scale-Up: Why Tablet Defects Appear When the Press Changes
Capping and lamination are classical scale-up issues. A formulation that makes sound tablets on a laboratory press can fail when the press, the speed, the unloading mode or the feed frame changes. Mazel and co-workers call these defects classical industrial issues that can be challenging during the scale-up of solid dosage forms. Each change in the list below shifts one term in the stress budget.
- Unloading mode — a rotary press unloads symmetrically, an eccentric press with a stationary lower punch unloads asymmetrically, and the simulator results differed accordingly.
- Press speed and dwell — slower compression or longer dwell allows more plastic deformation and a larger bonding area.
- Feed frame — shear in the feed frame adds lubrication that can cost tensile strength.
- Tooling — cup volume and clearance change how air is handled.
ICH Q8(R2) says that a design space proposed for several scales should be described in scale-independent parameters. Its example is shear rate in place of agitation rate for a shear-sensitive mixing step. The guideline adds that working within the design space is not a change, while moving outside it is a change that would normally start a post-approval process. A compression design space that records precompression pressure, press speed and ejection behaviour turns these studies into regulatory knowledge. Detection comes before correction, so the next section looks at the tests.
Detecting Tablet Defects: Friability, Breaking Force and Imaging
Visual inspection finds the defects that reach the surface and misses those that stay inside. Pharmacopoeial tests add mechanical stress to expose weak tablets, and imaging finds the cracks that the tests miss. The methods in the table cover different blind spots. Together they separate a sound tablet from one that will fail later.
| Method | What It Shows | Limit |
|---|---|---|
| Visual inspection | Cracks and caps on the surface | Central cracks in biconvex tablets can stay inside, and air-driven damage can be hidden |
| Friability, USP general chapter 1216 | Tumbling for 100 revolutions at 25 rpm; the sample fails if obviously cracked, cleaved or broken tablets are present, and a mean weight loss of not more than 1.0 percent is acceptable for most products | Covers compressed, uncoated tablets and supplements the breaking-force measurement |
| Breaking force, USP general chapter 1217 | The force needed to fracture the tablet, usually across its diameter | Lamination can interfere: the celecoxib tablets failed by lamination, so the study reported breaking force and not tensile strength |
| In-die elastic recovery | Air entrapment and stored elastic strain | Measured on a compaction simulator in the cited studies |
| X-ray microtomography | Internal cracks without breaking the tablet | Specialised equipment, which helps explain why internal defects are found late |
The USP text used here is the USP 38 reproduction, which states that it is harmonised with the European and Japanese pharmacopoeias. Check the current official chapter for acceptance criteria. Chapter 1217 also explains why the word hardness is misleading and why breaking force is the preferred term. Hidden internal defects are the reason a strength-versus-pressure curve deserves as much attention as the friability result. With detection in place, a team needs an order of operations.
Tablet Compression Troubleshooting: A Decision Sequence
Compression troubleshooting works best as a sequence that narrows the mechanism before anything changes. The location and timing of the defect show which family you face. Press settings and tooling are cheaper to change than a locked formulation, so they come before reformulation. The sequence below follows that logic.
- Locate the defect — crown separation points to capping and a split along the band to lamination. Powder on the punch face points to sticking, and missing material near an engraving to picking.
- Time it — check whether it appears at ejection or only after storage, handling or testing, because hidden cracks show late.
- Test for air — compare in-die elastic recovery with and without precompression, or add precompression and watch the breaking force.
- Test unloading and speed — slow the press or lengthen the dwell if throughput allows, and note whether the defect type changes.
- Check the tooling — cup depth, clearance, punch surface and debossing geometry.
- Review the lubrication — route and level across the full pressure range, including feed frame shear.
- Reformulate or re-granulate — powder deformation, binder and API engineering, if the earlier steps fail.
- Record the result — in the compression design space, with the pressure, speed and precompression settings that held.
The sequence keeps the cheapest and most reversible changes first and the composition change last. That order suits late-stage products, where the composition is locked and only the process can move.
Working With a Pharmaceutical Formulation Consultant
Tablet defects sit at the boundary between formulation, equipment and quality systems, so they rarely have a single owner. A pharmaceutical formulation consultant brings the compaction science, the press knowledge and the regulatory view into one plan. The aim is a tablet that stays intact from the press to the patient, backed by data. Pharmaceutical product development services then carry the plan into scale-up and validation.
- Defect diagnosis — classifying capping, lamination, sticking and picking by mechanism before changes are made.
- Compaction characterisation — elastic recovery, tabletability and precompression studies on a simulator.
- Lubrication strategy — lubricant choice, level and route balanced against strength and release.
- Tooling and press review — cup depth, clearance, surfaces and speed for the target press.
- Design space documentation — compression parameters recorded in the ICH Q8(R2) language.
- Technology transfer — contract formulation CDMO support with defined settings for the receiving press.
The full range of services sits under pharmaceuticals and health care. Before approaching a consultant, collect the press type, the tooling drawings and a photograph or cross-section of the failed tablets. Those three inputs show which family of defect you have.
Frequently Asked Questions
What are tablet defects?
Tablet defects are failures that appear during or after compression. They fall into two families: capping and lamination, where the compact cracks under stored elastic stress, and sticking and picking, where powder adheres to the tooling.
Each family has its own mechanism, so the fix for one can aggravate the other. More lubricant, for example, helps against sticking but can weaken the tablet.
What is the difference between capping and lamination?
Capping is the separation of the upper or lower crown of the tablet, usually during decompression or ejection. Lamination is a split of the tablet into layers along its band.
Researchers describe at least three lamination types: air entrapment, shear stress during ejection and tensile stress at the centre of biconvex tablets. The right fix depends on the type, which is why the two defects should not be treated as one.
Why do tablets laminate at high compression pressure?
Higher pressure can seal the surface of the compact so that air cannot escape, and it favours central tensile stress in biconvex tablets. In a celecoxib study, in-die elastic recovery rose to 13.5 percent at 200 MPa and the breaking force dropped at 350 MPa without precompression.
Lamination or capping is a common but not constant symptom of overcompression. A strength-versus-pressure curve that turns downward is the early warning, even when the tablets look sound.
How does precompression prevent capping and lamination?
Precompression applies a small first compression that removes air from the powder bed before the main compression. In the celecoxib study, 5 MPa of precompression cut elastic recovery from about 14 percent to about 4 percent at a main pressure of 350 MPa.
It is the most practical fix for air entrapment because it keeps throughput and is available on most rotary presses. It addresses Type 1 lamination only, so shear-driven or central-crack defects need other levers.
What causes tablet sticking and picking?
Sticking occurs when an API particle bonds more strongly to the punch than to its neighbours in the tablet. In a statistical analysis of 24 compounds, particle surface area and tablet tensile strength were the most significant factors.
Low-melting compounds that soften under frictional heat, hygroscopic powders and ductile materials all promote sticking. Picking is a specialised case in which powder is pulled away near debossed features, so engraving geometry and lubrication both matter.
Does more magnesium stearate stop sticking?
Not reliably. External lubrication of the punch with magnesium stearate worsened sticking at 50 MPa for sodium cyclamate, although sticking was absent at 200 MPa.
Internal lubrication also costs tensile strength and can prolong disintegration and slow dissolution. Judge any lubrication change across the full range of compaction pressures and check strength and release before accepting it.
Why do tablet defects appear after scale-up?
A new press changes the speed, the unloading mode, the tooling and the feed frame, and each shifts the stress budget of the compact. In a compaction-simulator study, symmetrical decompression, as on a rotary press, gave capping on both faces and lamination. Asymmetrical unloading suppressed lamination and limited capping to the upper face.
Feed frame shear can also act as extra lubrication and cost tensile strength. ICH Q8(R2) advises describing a design space across scales in scale-independent parameters, which helps carry the knowledge between presses.
How can a pharmaceutical formulation consultant help with tablet defects?
A consultant classifies the defect by mechanism, characterises the powder on a compaction simulator and recommends the lever that fits, whether precompression, tooling, lubrication or formulation. They also help record the settings in a design space.
Pharmaceutical product development services then cover scale-up, validation and transfer to the receiving press, including contract formulation CDMO support.
Fighting Capping, Lamination or Sticking on a Tablet Product?
Global Formulation supports pharmaceutical makers with defect diagnosis, compaction characterisation, lubrication strategy and technology transfer to a CDMO partner.
Talk to Our Formulation Team